
SOBRE NOSOTROS
Yantai Yunde Intelligent Technology Co., Ltd. cuenta con tan solo 30 años de experiencia en producción, ha prestado servicios a más de 300 clientes nacionales y extranjeros, y ha fabricado más de 2.000 máquinas.
SOLICITE UN PRESUPUESTO GRATUITO
-
Hogar

-
Blog
-
Blogs del sector
- How to Fix Common Steel Bar Straightening Problems

How to Fix Common Steel Bar Straightening Problems
-
autor
- 3,septiembre
 autor
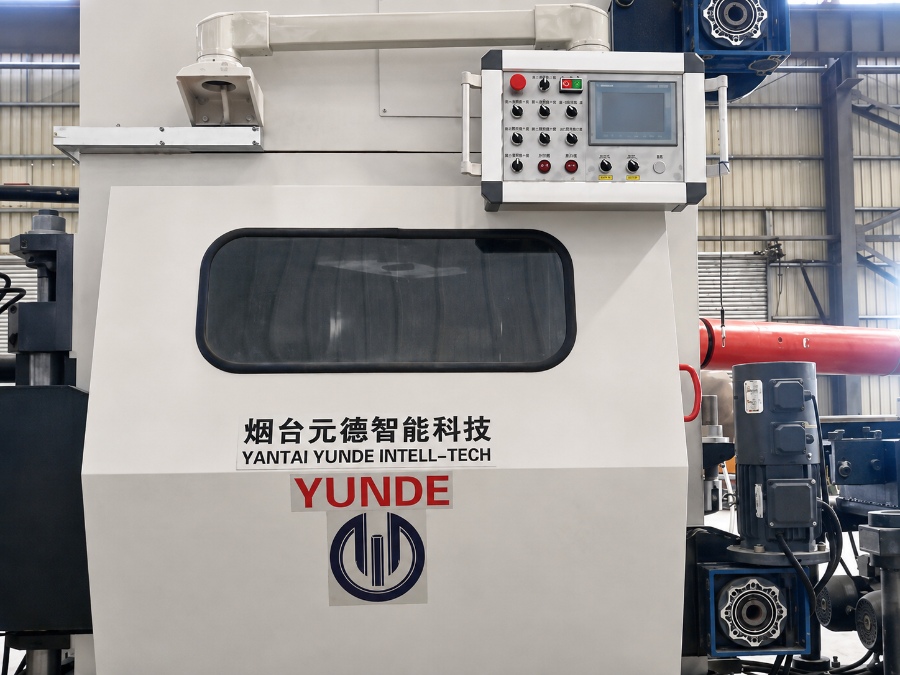
Steel bars can look straight yet fail inspection because of bow, diameter, or surface condition changes from end to end. A stable result comes from connecting the defect with roll pressure, guide alignment, entry material, and measurement. This guide keeps the focus on bar straightening so teams correct causes instead of repeatedly turning adjustment screws.
Why a straight bar can still fail inspection
A bar may look straight on a rack while its measured straightness varies along the length. Springback, end diameter change, or a contact mark can show that correction load was uneven. Inspect several positions and rotate the bar instead of relying on one sight line.
Entry diameter, length, alloy strength, and initial-bow direction set the correction window. When stock changes but the setting does not, a stable bar straightening process can produce alternating bends or end distortion.
Symptom patterns on finished bars
The defect pattern usually points to the first variable worth checking. Record the same locations after each change.
*One-sided bow: check guide centering and roll-gap symmetry.
*Residual curve: check springback compensation and material change.
*Waves or marks: check local reduction, roll cleanliness, and load stability.
*End shrinkage: check pressure release and end support.
A quick diagnosis before changing roll settings
Change one variable at a time and keep a reference bar. Measure the same positions before and after, then record feed speed and load. Use the table as a first diagnostic sequence, followed by a controlled trial.
| Observed Straightening Issue | Likely Cause | Recommended Inspection or Adjustment |
| One-sided bow | Guide or roll alignment | Measure gap and guide center at entry, middle, and exit |
| Wavy surface | Too much local reduction or unstable load | Inspect roll contact, load trend, and roll cleanliness |
| End diameter change | Pressure release or end support | Compare the first and last 200 mm with the middle section |
| Curve returns after release | Insufficient compensation for springback | Repeat the pass at a controlled load and speed |

Roll pressure and alignment control the correction
A two-row roller arrangement corrects the bar through repeated direction changes. Concave and convex rolls create linear contact along the length, distributing correction instead of concentrating it at one point. The resulting precision straightening roll system needs enough load to overcome the bend while keeping support and roll gap stable.
Constant pressure helps when material strength varies. A separate hydraulic system can hold and release load in sequence, while a rigid frame keeps the roll-gap position accurate and protects the machine during high-load correction.
Set correction around material behavior
High-strength bars often need gradual load increase because elastic recovery is greater. Start from the measured bend and stop when the result is stable; excess pressure can create end reduction, marks, or roll wear.
*Confirm diameter, length, and material grade.
*Center guides before fine roll adjustment.
*Verify straightness, diameter, and surface roughness together.
BS-series ranges that frame the adjustment decision
Model selection is part of defect prevention. A machine near the edge of its range leaves less room for stable support, so the BS model should cover the actual bar rather than only the nominal order size. The ranges below frame a round bar straightening machine trial.
| Modelo | Rango de diámetro (mm) | Longitud (m) | Speed (m/min) | Tolerancia de diámetro | Rugosidad superficial (μm) | Rectitud (mm/m) | Main Motor Power(kW) | Estructura |
| BS20 | Φ6–20 | ≥2 | 10–40 | ≤IT8 | Ra≤0,8 | 0.10 | 7.5×2 | Marco |
| BS40 | Φ10–40 | ≥2 | 10–35 | ≤IT8 | Ra≤0,8 | 0.15 | 22×2 | Marco |
| BS60 | Φ15–60 | ≥2 | 10–30 | ≤IT8 | Ra≤0,8 | 0.20 | 30×2 | Marco |
| BS80 | Φ20–80 | ≥2 | 10–24 | ≤IT8 | Ra≤0,8 | 0.25 | 37×2 | Marco |
| BS100 | Φ25–100 | ≥3 | 10–24 | ≤IT8 | Ra≤0,8 | 0.30 | 45×2 | Marco |
| BS130 | Φ35–130 | ≥3 | 10–20 | ≤IT8 | Ra≤0,8 | 0.35 | 75×2 | Marco |
| BS160 | Φ40–160 | ≥3 | 10–20 | ≤IT8 | Ra≤0,8 | 0.40 | 90×2 | Marco |
Process checks that prevent repeat defects
Yunde BS-series supports repeatable bar correction. A Máquina enderezadora de barras de acero page can help a technical team compare the BS range with its own diameter, length, speed, and straightness targets.
Production data closes the loop
A useful production record contains the model, material, diameter, length, feed speed, load or pressure setting, measured straightness, and the operator defect description. Over time, these records show whether a problem follows one material batch, one size, one guide position, or one speed range. That evidence is more valuable than a general claim that the line is running fast.
The same discipline supports a metal straightening production line review: define the target, measurement point, and handling checks so the bar is not re-bent.
When to stop adjusting and inspect the incoming bar
Repeated adjustment is not always the answer. If the defect returns after guides, load, and speed are checked, inspect incoming diameter spread, initial bow, and surface condition. A straightening unit cannot remove every upstream variation without added risk.
Escalate when the defect is concentrated at one end, appears only on one batch, or changes after handling. A controlled sample and clear measurement points show whether the straightening unit, material, or handling path needs attention.

A repeatable correction routine
A repeatable routine verifies material and model range, checks guides, sets pressure gradually, and measures several positions. The BS20–BS160 range covers Φ6–Φ160 mm bars with stated straightness values from 0.10 to 0.40 mm/m. Yunde can discuss the target through its technical consultation page.
Preguntas frecuentes
What causes a bar to leave a straightening machine with a one-sided bow?
A one-sided bow points to guide offset, unequal roll-gap alignment, or an off-center entry. Check the guide and gap before increasing load, then rotate a sample to separate runout from alignment.
How do I know whether roll pressure is too high?
Pressure is likely too high when end reduction, marks, rising load, or waviness appears without better straightness. Reduce the change and compare ends with the center.
What is the role of feed speed in bar straightening?
Feed speed changes contact time. A faster setting can reduce stability on strong or badly bent bars, so compare speed and load together.
Can a straightening machine handle high-strength bars?
Yes, when the model covers the bar and load, guides, speed, and verification are controlled. A straightening unit handling high-strength material needs gradual adjustment and closer springback monitoring.
Publicación reciente





Productos relacionados
Productos más vendidos

Línea de enderezamiento de bobina a barra
La varilla de alambre de acero inoxidable se desenrolla y se endereza previamente, luego se pela con un torno sin centros y se corta a la longitud precisa. Tras un último enderezamiento de precisión mediante una enderezadora de dos rodillos, el producto resultante es una barra recta de acero inoxidable de alta precisión.

Máquina peladora (torno sin centros)
La unidad de pelado (torno sin centros) es un producto desarrollado de forma independiente tras comparar las ventajas de productos extranjeros similares y combinarlas con las características de producción de las empresas nacionales, lo que dio como resultado un diseño simplificado y optimizado.

Línea de producción de bobina a bobina
La línea de producción de bobina a bobina es una serie de máquinas que incluyen una máquina desenrolladora y enderezadora, una máquina peladora, un mecanismo de sujeción, un dispositivo de precurvado, una máquina rebobinadora, etc. Mediante estas máquinas, la varilla de bobina negra se procesará para obtener una varilla de bobina brillante con una buena calidad superficial.

Máquina enderezadora serie BS
Una enderezadora es un dispositivo que se utiliza para enderezar perfiles, barras, tubos y alambres metálicos. La enderezadora utiliza rodillos enderezadores para comprimir el material y modificar su rectitud. Generalmente, cuenta con dos filas de rodillos enderezadores, con un número variable de ellos. También existen enderezadoras de dos rodillos, que se basan en el cambio de ángulo de dos rodillos (de forma cóncava e hiperbólica) para enderezar materiales de diferentes diámetros.

Máquina enderezadora de tubos de acero de rodillos múltiples
Es un dispositivo mecánico que se utiliza para corregir la curvatura y la ovalidad de las tuberías de acero. Se emplea para enderezar tuberías fabricadas con acero de alta aleación, resistente a la corrosión y al calor, así como con aleaciones de hierro-níquel, níquel y titanio, con el fin de reducir la falta de rectitud longitudinal y la falta de redondez transversal.

Máquina enderezadora horizontal y vertical
Suelte el volante de la enderezadora horizontal y vertical multirrodillo para que la bobina de alambre pase a través de los rodillos enderezadores. Apriete el volante hasta la posición determinada empíricamente, active el alimentador y realice varias pruebas de enderezamiento. A continuación, introduzca la bobina de alambre en los rodillos enderezadores verticales, siguiendo el mismo procedimiento que para el enderezamiento horizontal. Finalmente, introduzca la bobina de alambre en el alimentador de la desmoldadora.


