
SOBRE NOSOTROS
Yantai Yunde Intelligent Technology Co., Ltd. cuenta con tan solo 30 años de experiencia en producción, ha prestado servicios a más de 300 clientes nacionales y extranjeros, y ha fabricado más de 2.000 máquinas.
SOLICITE UN PRESUPUESTO GRATUITO
-
Hogar

-
Blog
-
Blogs del sector
- Bar Straightening for Precision Component Manufacturing
Bar Straightening for Precision Component Manufacturing
-
 autor
- 17,septiembre
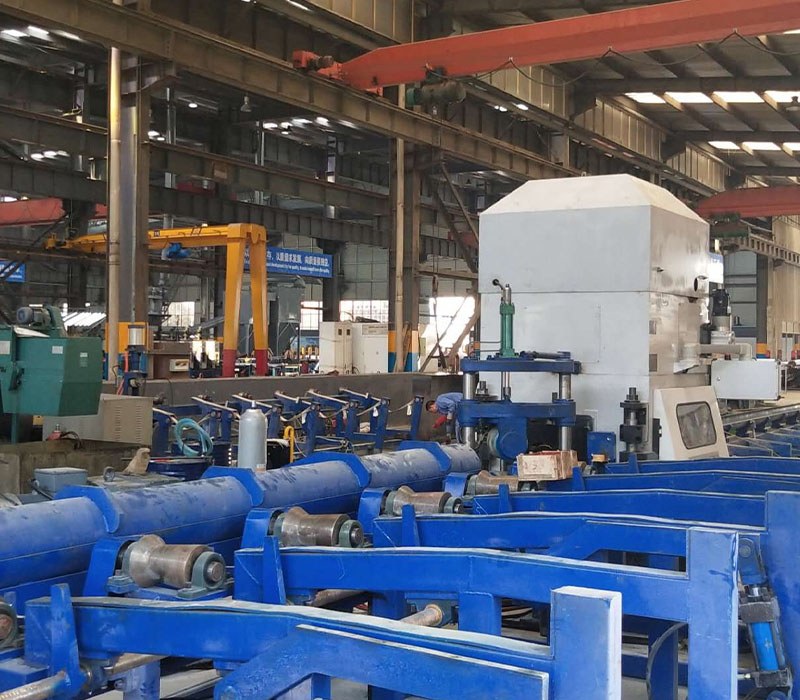
A bright round bar can have the right diameter and still cause trouble during machining. Bow changes how the stock sits, feeds and rotates. For processors supplying precision component manufacturers, straightening improves the geometry of the machining blank. Its value depends on how straightness, surface condition and material response relate to the next operation.
Why straightness matters before the first cut
Straightness describes the departure of a bar from a straight reference over a defined length. Diameter describes its cross-sectional size. A satisfactory diameter measurement therefore cannot establish whether a long bar is straight enough for its intended operation.
A bowed bar also leaves uneven material around the intended machining axis. Correcting that bow can make the available machining allowance more consistent. It does not create extra stock, repair internal defects or establish the final component’s dimensional tolerance.
Precision shafts make the distinction practical. A processor needs to supply stock that the component manufacturer can support and locate consistently. The customer’s drawing and process determine the required condition; a general description such as “precision bar” leaves too much unresolved.
This is the role of a round bar straightening machine in professional bar production: improving the geometry of the incoming blank before downstream operations have to accommodate it. Understanding how the correction happens explains why material and machine settings matter together.
How two rolls correct a curved bar
A two roll straightening machine works through controlled alternating bending and reverse bending as the bar moves through the roll contact region. Part of the deformation must remain after the load is removed. Purely elastic deflection would allow the bar to spring back toward its previous shape.
Roll contour, roll angle, roll gap and straightening speed influence that bending action. The relevant setting depends on the bar diameter and material response. Copying a setup from a different grade can produce a different result even when the nominal diameter is unchanged.
For processors evaluating this method, YUNDE’s BS series provides a frame-type, two-roll configuration for straight bars. Its concave and convex rollers use line contact, while the rigid overall frame helps maintain the roll-gap position. The BS series is the machine family discussed here.
An independent hydraulic system provides pressure holding and load release. These functions support controlled operation, but their presence alone does not establish the result for a particular batch. The useful evidence is the condition of representative bars after processing with the proposed setup.

What BS accuracy figures mean for machining stock
The BS80 provides a concrete example of how several specifications interact. Its processing diameter range is 20–80 mm, with a minimum bar length of 2 m and a listed speed range of 10–24 m/min. A short component blank below that minimum length falls outside this stated processing envelope.
Its listed straightness is 0.25 mm/m. To work together with the Yunde Peeling Machine and straightening machine, we can achieve bright bars with diameter tolerance ≤IT8 and surface roughness Ra≤0.8 μm.
| BS80 quality characteristic | Listed value | Meaning for the processor |
| Rectitud | 0,25 mm/m | Relates curvature to a stated length basis. |
| Tolerancia de diámetro | ≤IT8 | A tolerance grade, not a fixed millimetre allowance. |
| rugosidad superficial | Ra≤0,8 μm | Describes surface texture, not the bar’s longitudinal bow. |
The straightness entry requires a defined inspection method. Agree on the support arrangement, measured length, end treatment and acceptance criterion. Multiplying a per-metre figure by the total bar length does not, by itself, establish an allowable full-length bow or rotational runout.
A máquina enderezadora de barras should therefore be assessed against the drawing’s actual requirements. The BS80 example explains one processing envelope; it does not make that model the right choice for every combination of bar diameter, material strength and finished-component requirements.
Why a straight bar can still distort during machining
Straightening changes the material’s stress distribution as well as its shape. Research on two-roll straightening of 42CrMo bars has identified residual stress after the operation. A straight external profile should therefore never be presented as proof that a bar is free of internal stress.
Removing material during subsequent machining can disturb an existing stress balance. For a slender precision part, the practical question is whether the supplied stock stays sufficiently stable through the customer’s planned process. Straightness at dispatch answers only part of that question.
Representative trials should connect the straightened bar to its next operation. A useful trial records the material grade and condition, incoming curvature, machine setup, outgoing straightness and the result after the intended machining sequence. This ties the evaluation to an identifiable batch rather than a general capability claim.
Handling belongs in that evaluation too. Check bars after they have passed through the intended transfer and storage stages. The máquina alisadora establishes a processing step; the useful supply condition is the one that reaches the component manufacturer.
A clearer basis for precision bar supply
Bar straightening supports precision manufacturing by correcting the stock geometry that machining begins with. The strongest specification combines a defined straightness requirement with diameter, surface roughness and a material-specific trial. For the BS series, keep the selected model’s processing envelope and the customer’s downstream acceptance criteria in the same discussion.

Preguntas frecuentes
How does a two-roll machine straighten round bars?
The rolls impose bending and reverse bending through their contact with the moving bar. Controlled permanent deformation reduces the remaining curvature after unloading. Roll geometry and settings influence the result.
Is straightness the same as diameter tolerance?
No. Straightness concerns longitudinal form; diameter tolerance concerns cross-sectional size. A bar can satisfy one requirement while missing the other, so both need separate evaluation.
What straightness is listed for the BS80?
The BS80 has a listed straightness of 0.25 mm/m. Confirm the inspection method, material condition and agreed acceptance criteria before treating that entry as a production commitment.
Does straightening remove all residual stress?
No such conclusion follows from a straightness measurement. Two-roll straightening can leave residual stresses, so demanding precision applications may need trials through the subsequent machining process.
Can the BS80 process short component blanks?
Its stated minimum bar length is 2 m. A shorter blank is outside that listed envelope. Evaluate the appropriate stock-processing stage and model configuration before assuming it can be handled.
Publicación reciente





Productos relacionados
Productos más vendidos

Línea de enderezamiento de bobina a barra
La varilla de alambre de acero inoxidable se desenrolla y se endereza previamente, luego se pela con un torno sin centros y se corta a la longitud precisa. Tras un último enderezamiento de precisión mediante una enderezadora de dos rodillos, el producto resultante es una barra recta de acero inoxidable de alta precisión.

Máquina peladora (torno sin centros)
La unidad de pelado (torno sin centros) es un producto desarrollado de forma independiente tras comparar las ventajas de productos extranjeros similares y combinarlas con las características de producción de las empresas nacionales, lo que dio como resultado un diseño simplificado y optimizado.

Línea de producción de bobina a bobina
La línea de producción de bobina a bobina es una serie de máquinas que incluyen una máquina desenrolladora y enderezadora, una máquina peladora, un mecanismo de sujeción, un dispositivo de precurvado, una máquina rebobinadora, etc. Mediante estas máquinas, la varilla de bobina negra se procesará para obtener una varilla de bobina brillante con una buena calidad superficial.

Máquina enderezadora serie BS
Una enderezadora es un dispositivo que se utiliza para enderezar perfiles, barras, tubos y alambres metálicos. La enderezadora utiliza rodillos enderezadores para comprimir el material y modificar su rectitud. Generalmente, cuenta con dos filas de rodillos enderezadores, con un número variable de ellos. También existen enderezadoras de dos rodillos, que se basan en el cambio de ángulo de dos rodillos (de forma cóncava e hiperbólica) para enderezar materiales de diferentes diámetros.

Máquina enderezadora de tubos de acero de rodillos múltiples
Es un dispositivo mecánico que se utiliza para corregir la curvatura y la ovalidad de las tuberías de acero. Se emplea para enderezar tuberías fabricadas con acero de alta aleación, resistente a la corrosión y al calor, así como con aleaciones de hierro-níquel, níquel y titanio, con el fin de reducir la falta de rectitud longitudinal y la falta de redondez transversal.

Máquina enderezadora horizontal y vertical
Suelte el volante de la enderezadora horizontal y vertical multirrodillo para que la bobina de alambre pase a través de los rodillos enderezadores. Apriete el volante hasta la posición determinada empíricamente, active el alimentador y realice varias pruebas de enderezamiento. A continuación, introduzca la bobina de alambre en los rodillos enderezadores verticales, siguiendo el mismo procedimiento que para el enderezamiento horizontal. Finalmente, introduzca la bobina de alambre en el alimentador de la desmoldadora.


